info@starmodul.com

E-mail de contacto

973 228 164 / 683 442 608

Teléfono de soporte

TECHNICAL INFORMATION · PRODUCTION

Sandwich panel manufacturing: production process

Sandwich panel manufacturing combines chemical dosing, forming of the metal faces, formation or incorporation of the core, pressing, curing, cutting, stacking, and packaging. The original technical page distinguishes between batch systems and continuous production lines.

This version preserves all the historical technical parameters of the original page, but expressly identifies the data that must be interpreted as process reference and not as universal performance of any current factory or panel.
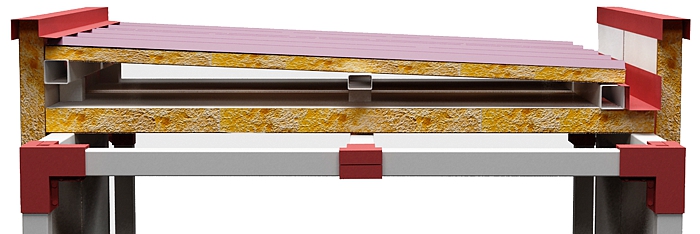
Technical section on sandwich panel and core configuration

Sandwich panel manufacturing principles

Manufacturing combines continuous materials—such as coil sheet—with a core that can be formed chemically during the line or incorporated as a rigid material previously produced. Process control seeks to maintain mixing, adhesion, geometry, and finish in a repeatable manner.

Reactive material

Polyol + polyisocyanate

Manufacturers receive liquid components and convert them into polyurethane through a controlled reaction, together with additives defined by formulation.

Dosing

Precision and temperature

The viscosity and proportion of the components affect the mixture. For this reason, tanks, pumps, and control circuits are a critical part of the process.

Formation

Continuous or batch

Manufacturing can be carried out in closed molds per panel or in automatic lines where the panel is formed, cured, cut, and stacked continuously.

Materials and Finished Product

Beyond the process overview, it is useful to see how materials become the finished product and how geometry changes according to the application.

Technical section: roof sandwich panel

Panel Section

The final geometry integrates the two faces, the insulating core, and the joint formed during production.
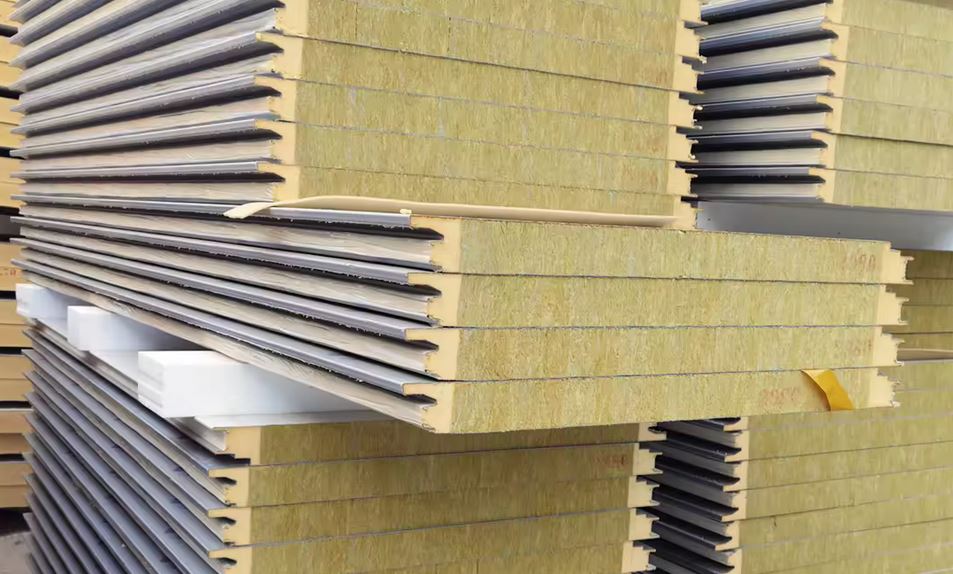
Stacked rock wool sandwich panels

Finished and Stacked Panel

Edge finishing and package stability are important before transport.
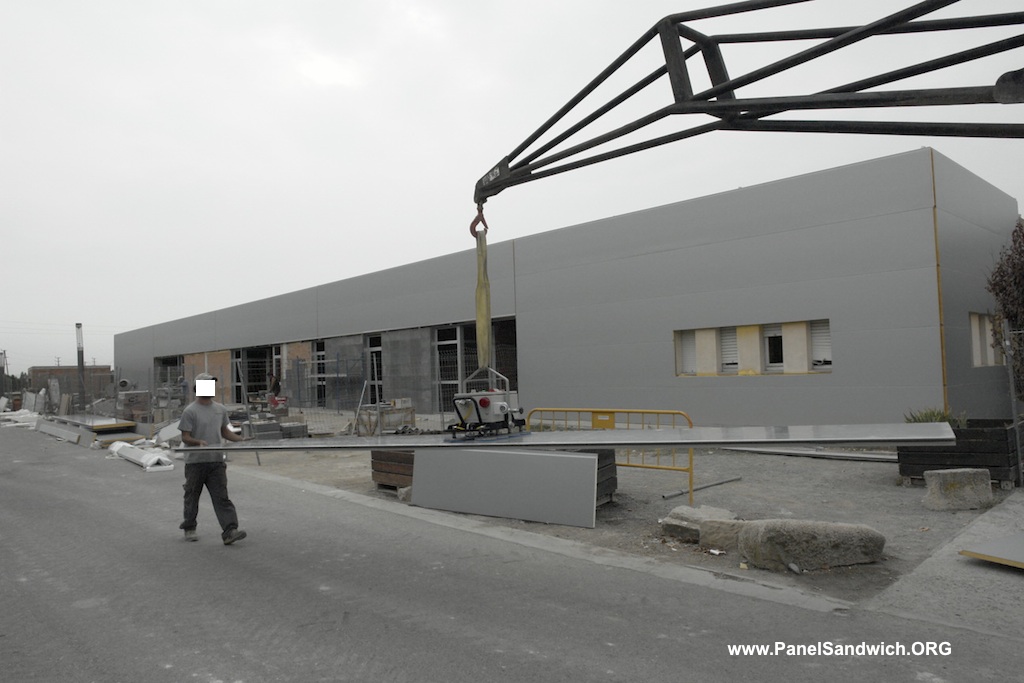
Handling of facade sandwich panels

Product Handling

Length, rigidity, and surface finish determine the unloading and handling of the manufactured panel.

Reaction injection molding (RIM): dosing and mixing

The original page calls reaction injection molding (RIM) the process based on a high-pressure foaming unit. In this system, polyol, polyisocyanate, and additives are combined to generate a reactive mixture capable of forming microcellular or microporous foams in reduced cycle times.

Storage tanks and day tanks

The main components and additives—stabilizers, flame retardants, pigments, and others—are kept in storage tanks and transferred before production to feed tanks or day tanks.

Thermal control is important because a temperature variation, especially in polyols, modifies viscosity. The source describes double-walled tanks, with stirrer and temperature control circuits to maintain process conditions as constant as possible.

Recirculation before injection

Before each mixing and filling cycle, the components recirculate in the required proportions and at the required pressure. Electronically controlled actuators divert the flow from the recirculation circuit to the injection circuit and then restore recirculation.

Context: the description corresponds to the technical system recorded in the original page. Formulation, temperature, pressure, and machine architecture must be verified for each actual production line.

Dosing pumps: precision, flow rate, and limitations

Dosing must be repeatable and precise. The objective of the pumps is to transport from the day tanks to the foaming head the correct quantity of each component, maintaining the intended mixing ratio.

The historical source cites flow rates of 12 to 150 liters per minute for axial piston pumps, highlighting their low noise level and precision. It also indicates two limitations: high-viscosity liquids and the presence of abrasive fillers.

ElementHistorical dataFunction / limitation described
Dosing pumps12–150 L/minThe source cites axial piston pumps of high precision to reproduce mixing ratios.
ViscosityQualitative limitationAxial piston pumps have limitations when liquids have high viscosities.
Abrasive fillersNot recommended in the described configurationThe source warns that liquid components must not contain abrasive fillers for this pumping system.
Head nozzles100–150 m/sHistorical velocity cited for the components through the injection nozzles.

High-pressure foaming head

The foaming head is the point at which the components meet and mix. The technique described uses high-pressure impingement: the liquids are injected into the mixing chamber and their kinetic energy promotes intimate mixing.

The original page cites component velocities in the nozzles of approximately 100–150 m/s.

Piston cycle and recirculation

  1. In recirculation position, the components return to the tanks through small ducts.
  2. When the piston is withdrawn, the mixing chamber opens and the components impinge on each other.
  3. When the piston advances again, mixing is interrupted.
  4. Recirculation is restored and the remaining reactive mixture is removed from the chamber.

This mechanism allows synchronization of mixture supply, especially in batch processes.

Production facilities and equipment

The system described integrates the mixing/injection machine, the mold or press, and the auxiliary equipment necessary to form, cut, and handle the panel.

EquipmentFunction within the system described
Feed tanksKeep the components available under controlled thermal conditions.
Dosing / recirculation pumpsControl flow rate, proportion, and circulation prior to mixing.
Foaming headMixes the components by high-pressure injection.
Mold or pressDefines geometry and maintains the faces during expansion and hardening.
Auxiliary equipmentProfiling, heating, cutting, stacking, packaging, and automation according to line type.

Batch system

Each panel is manufactured in a closed mold of the final dimensions.

  • Allows more complex geometries.
  • Can favor surface finish.
  • Accepts alternative starting materials.
  • Lower production rate.

Continuous system

The faces advance from coils and the panel is formed continuously.

  • Oriented to large productions.
  • Profiling, preheating, and foaming in-line.
  • Double-belt press.
  • Cutting, stacking, and packaging can be automated.

Batch production: mold molding

In mold molding, the panel is produced in a closed cavity whose dimensions correspond to those of the finished panel. The mold has a solid lower structure and a lid, and must withstand the pressures generated during foam solidification.

  1. The already profiled metal faces are placed inside the mold.
  2. The lower face rests on the bottom and the upper one is held in position by lateral supports.
  3. The lid is closed.
  4. An exact quantity of foam is introduced through a lateral nozzle; the source indicates that this operation lasts only a few seconds.
  5. After foaming, the panel remains in the mold approximately 40 minutes.
  6. The panel is removed and the mold is prepared for the next cycle.

Historical advantages cited: possibility of manufacturing complicated shapes, good exterior appearance, and use of alternative initial materials. Main disadvantage: relatively low production speed.

Continuous production: complete line sequence

1

Uncoiling

Two coils supply the upper and lower metal faces.

2

Profiling

Rollers form the surface relief and edge details.

3

Preheating

The historical source cites approximately 40°C before introducing the foam.

4

Foam dosing

The high-pressure mixture is distributed in an oscillating manner over the lower face.

5

Double-belt press

Acts as a moving mold, controls face separation, and resists expansion pressure.

6

Curing / adhesion

PUR/PIR adhere to the faces while the assembly advances through the press.

7

Cutting

The hardened panel is cut to the required length by saw.

8

Stacking and packaging

The panels are grouped and protected for shipment.

From Profiling to Installed Panel

The result of the continuous line changes depending on the exterior profile, the joint solution, and the panel’s final application.
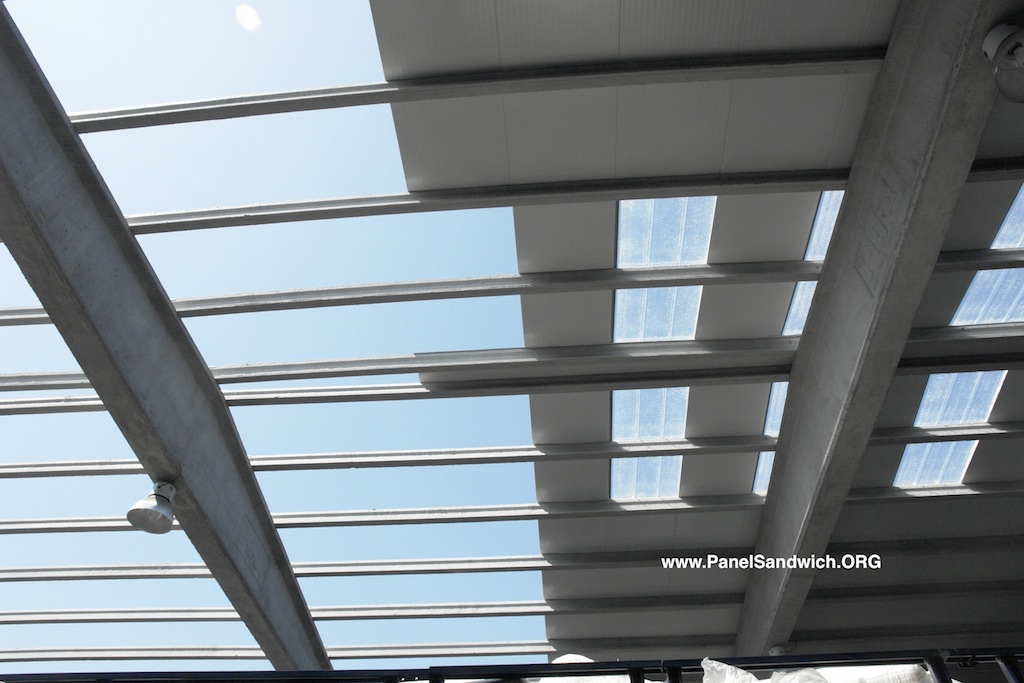
Installed five-rib roof sandwich panel

Roof Profiling

The ribs are formed during the profiling of the faces and provide geometry to the finished product.
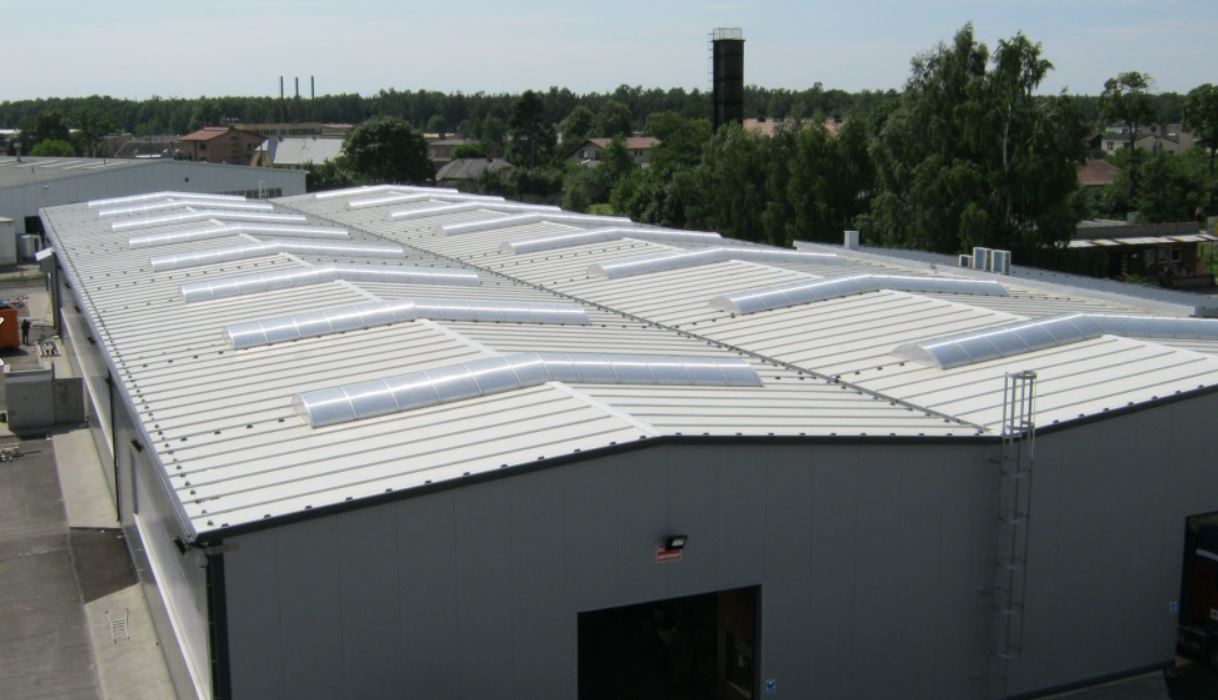
Roof made with sandwich panel

Panel Continuity

Production’s dimensional precision facilitates alignment, overlap, and continuity on site.
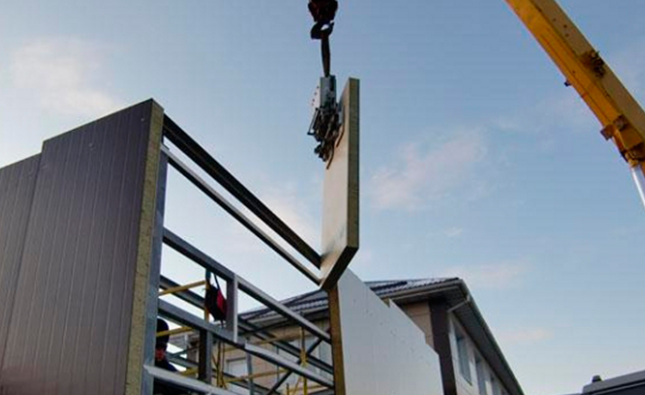
Sandwich panel assembly on structure

From Package to Site

Cutting to length and packaging must facilitate transport, lifting, and placement without damaging the faces.

Coils, profiling, preheating, and double-belt press

For large volumes, the original page describes automatic continuous foaming lines. The two sheets are unwound from coils and pass through rollers that generate the surface profile and panel edges.

They are then preheated to approximately 40°C, a historical datum associated in the source with optimal foam adhesion. The reactive mixture generated by the high-pressure equipment is deposited by an oscillating movement onto the lower face before entering the double-belt press.

Double-belt press

The press functions as a moving mold: it resists foam pressures during hardening and maintains the two faces at the necessary distance. In this section the foam also adheres to the upper profiled face.

The source highlights the high adhesive capacity of PUR/PIR on the surfaces with which they come into contact. Upon leaving the press, the core has already hardened sufficiently to cut the panel to size.

The ~40°C corresponds to the process described in the original source. The effective temperature of a current line depends on formulation, sheet, adhesion, speed, and manufacturer specification.

Cutting, stacking, and packaging

Cutting

The hardened continuous panel is cut to the necessary length with a saw. The original page mentions a band saw as a reference for the line described.

Stacking

Each panel passes to a stacking machine. In heavily profiled roof panels, the source describes an alternating arrangement to optimize package height: outer faces facing each other on one side and inner faces facing each other on the other.

Packaging

The package is protected with stretch polyethylene film, applied by a ring-shaped rotating wrapper.

Historical production line parameters

The source directly relates line speed to final thickness: the greater the thickness, the more time the panel needs in the double-belt press to complete adhesion and, therefore, the lower the speed must be.

On the figure of 500,000 m² per shift: it is preserved because it appears in the historical documentation of this page. It must be treated as data inherited from the source, not as a capacity specification of a current line. Actual production depends, among other factors, on usable width, shift duration, stops, thickness, formulation, and effective speed.
Parameter from the original pageValueHow it should be interpreted
Face preheating≈40°CReference from the line described; not a universal value.
Average speed cited6 m/minHistorical example of installation speed.
General speed range2–15 m/minThe source indicates that it decreases as thickness increases due to longer dwell time in press.
Capacity cited≈500,000 m² in one shiftFigure reproduced from historical content. Must be verified for any actual installation and is not presented as universal capacity.
Batch molding≈40 min in moldHistorical time of the system described.

Production of panels with mineral wool

When the core is mineral wool—or another rigid material in the systems described—the original page indicates that the general line concept is maintained, but the core preparation and the method of bonding to the faces change.

Cutting into strips

One solution consists of cutting the slab into strips at right angles to the fiber orientation. The width of each strip matches the desired panel thickness.

90° rotation

The strips are rotated 90 degrees so that the fibers are oriented approximately normal to the outer faces. The source links this arrangement with the final compression and tensile properties of the composite panel.

Use of complete slab

The page also mentions, as a technique under development at the time of writing, the use of the complete mineral wool slab. That phrase is preserved as a historical reference and is not presented as a current innovation.

Staggering of strips

The joints between strips are arranged staggered to prevent all cutting planes from coinciding in the same cross section, since that coincidence could significantly deteriorate the shear strength of the assembly.

Adhesives for bonding the mineral core to the faces

The bond between the mineral wool strips and the metal faces is made with an adhesive suitable for the composition of the materials and the manufacturing process.

The adhesion phase is completed during the panel’s passage through the double-belt press.

Fire behavior: the original text attributes significant fire resistance to panels manufactured with mineral wool. In this version the historical idea is maintained, but the current performance must be expressed through the tested classification of the complete panel; it must not be deduced solely from the core or the adhesive.
Type of adhesive citedApplication / curingAdvantage describedLimitation described
Solvent-basedSprayed on both surfaces; curing can be accelerated with slight pressure and temperature.Simple handling and good adhesion characteristics.Once the layers are bonded, the relative position cannot be corrected.
Epoxy or polyurethane resin, 2 componentsComponents mixed in situ; after a preset time they react and harden rapidly.Allows correction of layer position before hardening.The layers must be kept under pressure for a specified period.

Mineral Wool Panels: Process Result

In mineral wool panels, the core’s orientation and its bonding to the faces are especially relevant for the final performance.
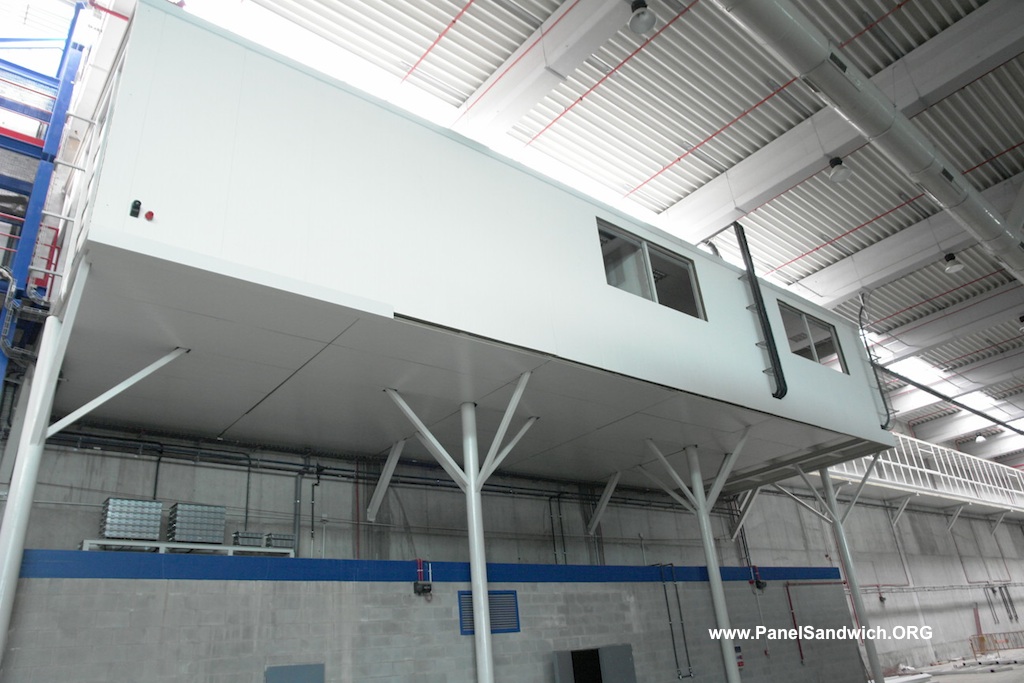
Interior enclosure with rock wool sandwich panel

Mineral Wool Panel

The finished product must maintain joint continuity and dimensional stability.
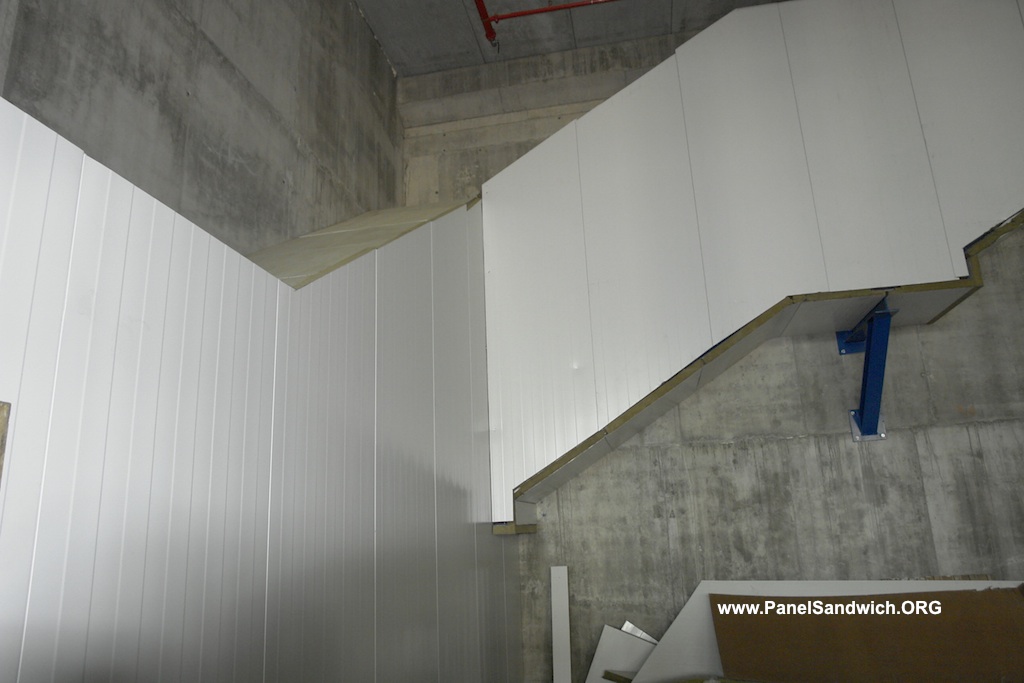
Rock wool sandwich panel installed in enclosure

Junctions and Cuts

The produced geometry must allow for resolving system junctions, openings, and finishes.
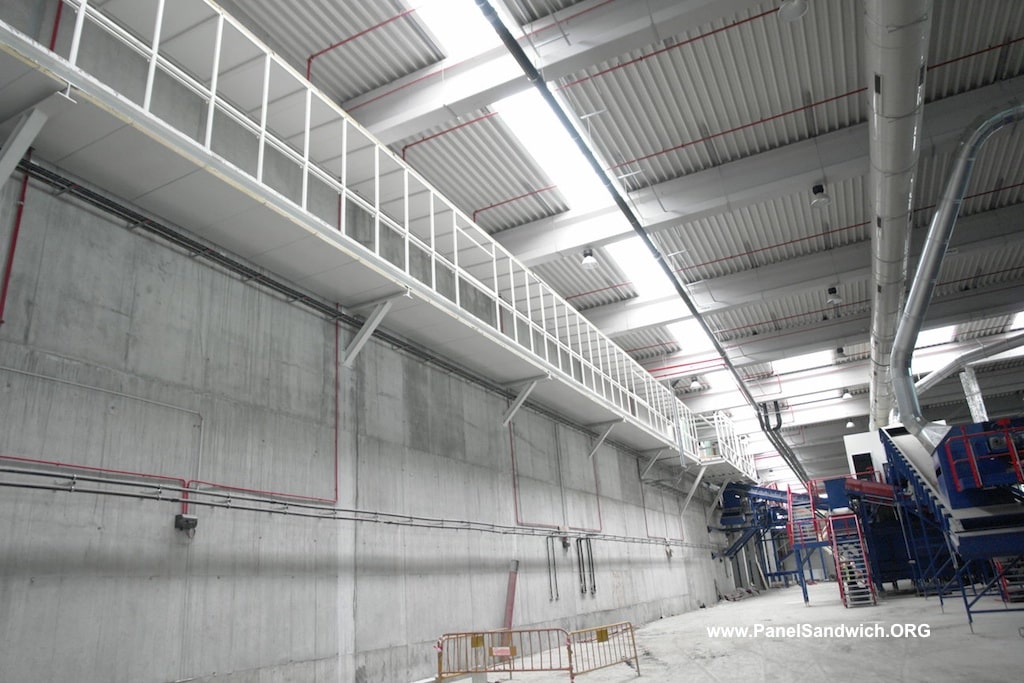
Warehouse interior with rock wool sandwich panel

Result on Large Surfaces

The repeatability of width, thickness, and joint becomes visible in long enclosures.

What actually controls repeatable production

Chemical dosing

  • Ratio between components
  • Temperature and viscosity
  • Pump flow rate
  • Recirculation and injection

Geometry

  • Face profiling
  • Press separation
  • Thickness
  • Edge / joint details

Adhesion and core

  • Uniform distribution
  • Sufficient curing
  • Strip orientation
  • Core continuity

Finished product

  • Cutting length
  • Surface appearance
  • Stacking / protection
  • Traceability and defined controls

This page explains the manufacturing principle. Acceptance criteria, tolerances, and product performance must be consulted in the technical documentation and quality control applicable to the specific panel.

From process to finished product

Technical configuration of roof sandwich panel

Product geometry

The line must maintain thickness, face profile, and joint configuration in a repeatable manner.

Rock wool sandwich panel with visible core

Mineral wool core

The orientation and arrangement of the strips is part of the production process of the mineral panel.

Sandwich panel handled on site

From packaging to site

Stacking and final protection must allow the panel to be transported without damaging faces, edges, or joints.

Continue with the technical guide

After understanding production, it is advisable to review coatings, quality control, handling, and performance of the finished panel.

Frequently asked questions about sandwich panel manufacturing

The original page uses the term reaction injection molding for the high-pressure mixing and injection system of polyol, polyisocyanate, and additives. The components are dosed, recirculated, and mixed in a head before forming the foam.

In the batch system each panel is formed inside a closed mold. In the continuous system, the metal faces advance from coils through profiling, preheating, foaming, double-belt press, cutting, and stacking.

The historical source cites an approximate preheating of 40°C to favor adhesion. It should not be taken as a universal setpoint: the actual temperature depends on the formulation and the line.

According to the original content, a thicker panel needs to remain longer inside the press to adequately complete curing and adhesion of the core to the faces.

One technique described cuts the slab into strips, rotates them 90°, and arranges them staggered. They are then adhered to the metal faces and the assembly passes through the press.

No. They are historical references from the original source. The actual capacity of a line depends on width, thickness, formulation, shift duration, stops, and equipment configuration.